- International Standard
- Material Grades
- Outer Diameter
- Wall Thickness
- Surface
- Tube Type
- Mill Test Certificate(MTC)
- Certificate
- AS1528.1
- AISI 304/304L/316/316L
- 12.7mm – 219.1mm
- 1.20mm – 2.60mm
- Grit 180, 240, 320
- Welded , Seamless
- EN10204 3.1
- ISO 9001:2015 , PED 2014/68/EU , AD 2000-WO
- 6.35mm - 304.8mm
- 0.89mm - 3.05mm
- ≤20Ra (0.5 μm) ID ≤30Ra (0.8 μm) OD
AS1528.1 Stainless Steel Sanitary Tubes
- International Standard
- Material Grades
- Outer Diameter
- Wall Thickness
- Surface
- Tube Type
- Certificate
- AS1528.1
- AISI 304/304L/316/316L
- 12.7mm – 219.1mm 6.35mm - 304.8mm
- 1.20mm – 2.60mm
- Grit 180, 240, 320≤20Ra (0.5 μm) ID ≤30Ra (0.8 μm) OD
- Welded , Seamless
- ISO 9001:2015 , PED 2014/68/EU , AD 2000-WO
AS 1528.1 sanitary tube covers stainless steel tubing used in hygienic food and dairy processing equipment. It provides requirements for tube materials, dimensions, tolerances, manufacture, surface condition, and testing so that tubing can be selected for cleanable process lines and compatible sanitary fittings.
Project specifications should identify the required stainless steel grade, outside diameter, wall thickness, length, manufacturing route, and internal and external finish. The appropriate surface condition depends on the product being transferred, cleaning procedure, fabrication method, and customer documentation requirements.
For alternative sanitary specifications, compare ASTM A270 sanitary tubing and EN 10357 sanitary tubing, or browse the full stainless steel sanitary tubing range. To request a quotation, send the standard, grade, dimensions, finish, quantity, and destination.
Dimension of AS1528.1 Stainless Steel Sanitary Tubes
| Size OD | Tolerance of OD | Wall Thickness | Tolerance on Wall Thickness | Tolerances on Length | Weight KG/M |
|---|---|---|---|---|---|
| 12.70 | +/- 0.1 | 1.20 | +/- 10.0% | +3, -0 | 0.344 |
| 15.88 | +/- 0.1 | 1.20 | +/- 10.0% | +3, -0 | 0.439 |
| 19.05 | +/- 0.1 | 1.20 | +/- 10.0% | +3, -0 | 0.534 |
| 25.40 | +/- 0.1 | 1.60 | +/- 10.0% | +3, -0 | 0.949 |
| 38.10 | +/- 0.1 | 1.60 | +/- 10.0% | +3, -0 | 1.103 |
| 50.80 | +/- 0.1 | 1.60 | +/- 10.0% | +3, -0 | 1.455 |
| 63.50 | +/- 0.1 | 1.60 | +/- 10.0% | +3, -0 | 1.961 |
| 76.20 | +/- 0.1 | 1.60 | +/- 10.0% | +3, -0 | 2.467 |
| 101.60 | +/- 0.1 | 1.60 | +/- 10.0% | +3, -0 | 2.973 |
| 114.30 | +/-0.38 | 2.00 | +/- 10.0% | +3, -0 | 5.595 |
| 139.70 | +/-0.38 | 2.00 | +/- 10.0% | +3, -0 | 6.860 |
| 168.30 | +/-0.76 | 2.60 | +/- 10.0% | +3, -0 | 10.732 |
| 219.10 | +/-1.55 | 2.60 | +/- 10.0% | +3, -0 | 14.022 |
Finish Specifications
The standard mandates that the interior surface must be smooth, non-toxic, non-absorbent, and corrosion-resistant. This is primarily achieved through a mechanical polishing and electropolishing process. The result is an ultra-smooth finish that minimizes the ability for microbes and product particles to adhere, and it allows for effective cleaning and sterilization.
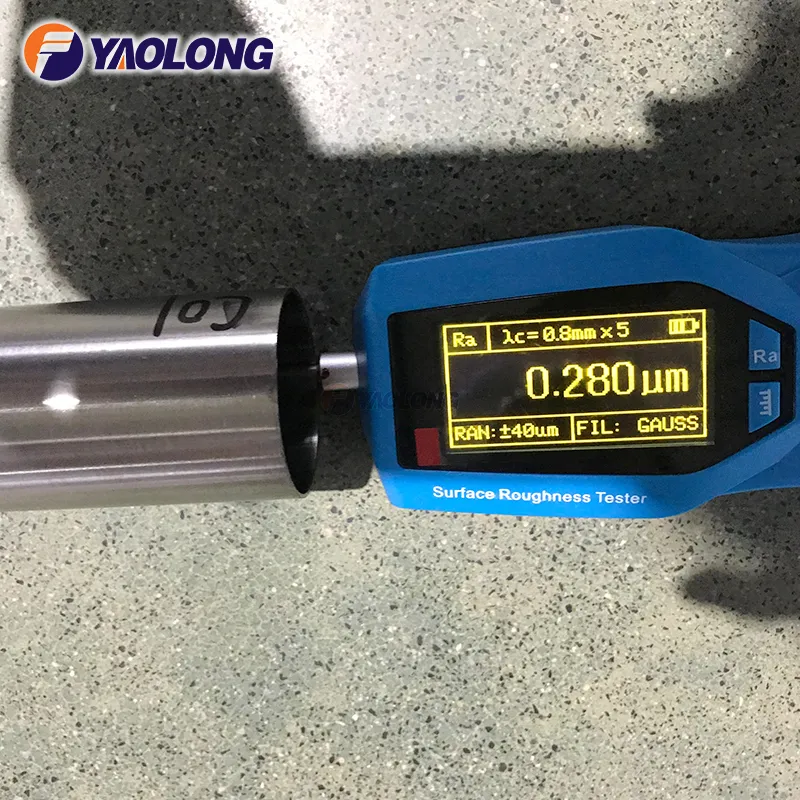
The most common and accepted finish is defined by a maximum Ra (Roughness Average) value. A typical Ra specification for ASTM A270 tubing is ≤ 0.38 µm (15 microinches) or better, often referred to as a “sanitary finish” or “micro-finish.” Some applications, like high-purity pharmaceutical or biotech processes, may require an even smoother finish of ≤ 0.25 µm (10 microinches).
This smooth surface is created by first mechanically abrading the tube with progressively finer abrasives to remove imperfections and weld beads. This is often followed by electropolishing, an electrochemical process that removes a thin layer of surface material. Electropolishing further smooths the surface, removes embedded contaminants, and enhances the natural passive oxide layer, which significantly improves corrosion resistance.
The primary purpose of this meticulously controlled surface is to prevent contamination, facilitate easy and effective cleaning-in-place (CIP) and sterilization-in-place (SIP) procedures, and provide superior corrosion resistance against aggressive cleaning chemicals and process fluids.
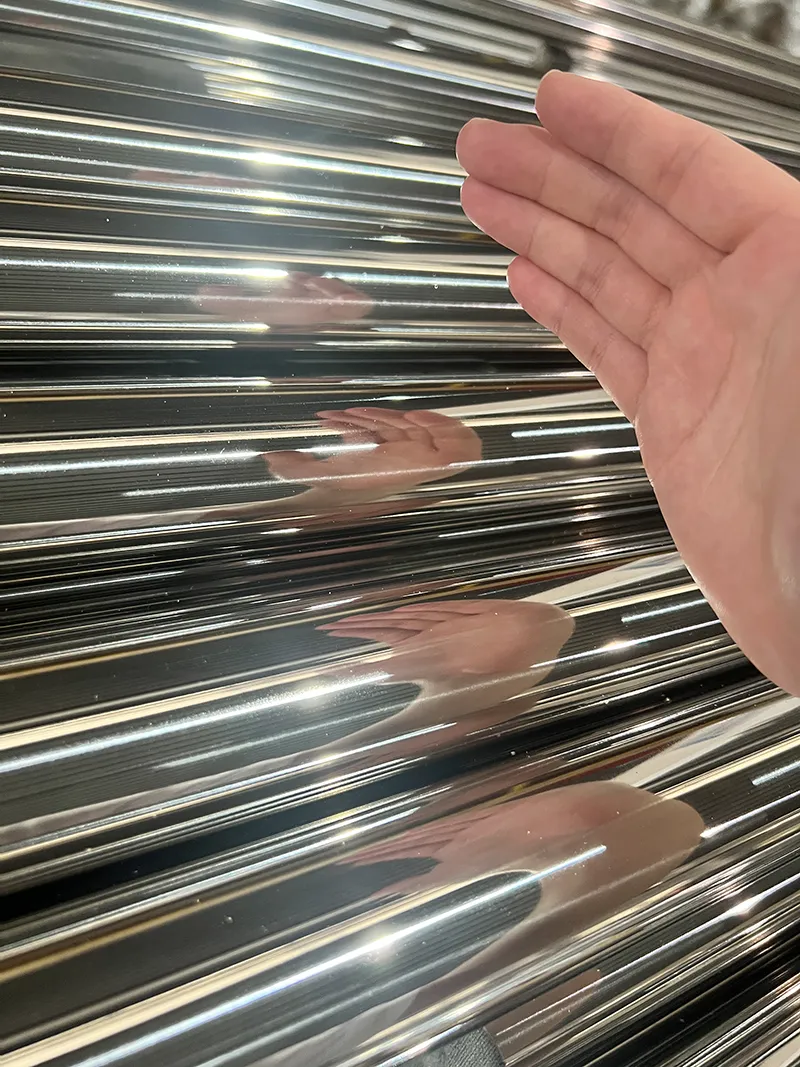
Mirror Polished Surface
| Process | RA Micro Inch | RA Micron | ISO Designation |
|---|---|---|---|
| 150 grit | 30-35 | 0.75-0.875 | N6 |
| 150 grit + Electropolish | 12-20 | 0.3-.05 | |
| 180 grit | 20-25 | 0.5-.0625 | |
| 180 grit + Electropolish | 10-16 | 0.25-0.4 | |
| 240 grit | 15-20 | 0.375-0.5 | N5 |
| 240 grit + Electropolish | 8-12 | 0.2-0.3 | |
| 320 grit | 8-12 | 0.2-0.3 | N4 |
| 320 grit + Electropolish | 6-12 | 0.15-0.3 |
Chemical Composition of Stainless Steel Tubes
| TUBE GRADES | UNS | Cr | Ni | Mo | C | P | S | Mn | Si |
| TP304 | S30400 | 18.0-20.0 | 8.0-11.0 | – | 0.08 | 0.045 | 0.03 | 2 | 1 |
| TP304L | S30403 | 18.0-20.0 | 8.0-13.0 | – | 0.035 | 0.045 | 0.03 | 2 | 1 |
| TP316 | S3160 | 16.0-18.0 | 11.0-14.0 | 2.0-3.0 | 0.08 | 0.045 | 0.03 | 2 | 1 |
| TP316L | S31603 | 16.0-18.0 | 10.0-14.0 | 2.0-3.0 | 0.035 | 0.045 | 0.03 | 2 | 1 |
Tensile Properties of Stainless Steel Tubes
| Material | Heat Treatment | Yield Strength | Tensile Strength (MPa) | Temperure | Elongation %, Min |
| Ksi (MPa), Min. | Ksi (MPa), Min. | Min. º F(º C) | |||
| ASME SA270 304 | Solution | 30(205) | 75(515) | 1900 (1040) | 35 |
| ASME SA270 304L | Solution | 25(170) | 70(485) | 1900 (1040) | 35 |
| ASME SA270 316 | Solution | 30(205) | 75(515) | 1900(1040) | 35 |
| ASME SA270 316L | Solution | 25(170) | 70(485) | 1900(1040) | 35 |
Manufacturing Process The manufacturing process of ASTM A270 sanitary tubing, commonly used in hygienic applications like food, beverage, pharmaceutical, and dairy industries, involves several key steps to ensure high cleanliness, corrosion resistance, and smooth internal surfaces. Here’s a detailed breakdown: 1. Material Selection – Grades: ASTM A270 covers austenitic stainless steels (e.g., 304/304L, 316/316L) and ferritic steels (e.g., 444). – Form: Starts with high-quality stainless steel coils or hollow billets. 2. Tube Formation 2.1 Welded Tubes (Most Common for Sanitary Applications) – Cold Rolling/Strip Preparation: Stainless steel strips are precision-rolled to required thickness. – Forming: The strip is fed into a tube mill and gradually shaped into a cylindrical form via rollers. – Welding: – TIG (Tungsten Inert Gas) Welding: Used for high-purity applications; ensures a smooth, contamination-free weld. – Laser Welding: For ultra-precise, minimal-heat-affected zones. – Weld Seam Annealing & Polishing: The weld is annealed (heat-treated) to restore corrosion resistance and polished to match the parent material. 2.2 Seamless Tubes (Less Common, Higher Pressure Applications) – Extrusion/Piercing: A billet is heated and pierced to form a hollow shell. – Cold Drawing: The tube is drawn through dies to achieve precise dimensions and smooth surfaces. 3. Heat Treatment (Annealing) – Tubes are annealed at 1900–2050°F (1040–1120°C) to relieve stresses and restore corrosion resistance. – Rapid cooling (quenching) prevents carbide precipitation (critical for 316L/304L grades). 4. Finishing & Surface Treatment – Pickling & Passivation: Acid bath (nitric/hydrofluoric) removes oxide layers and enhances chromium oxide passive layer. – Electropolishing (Optional): Electrochemical process removes surface imperfections, improving cleanliness and corrosion resistance. 5. Internal Polishing – Mechanical Polishing: Abrasive belts/buffing for Ra ≤ 15 µin (0.38 µm) or smoother (common for 3A sanitary standards). – Electropolishing (Optional): Achieves Ra ≤ 5 µin (0.13 µm) for ultra-hygienic applications. 6. Cutting & End Finishing – Precision-cut to length with square-cut ends or beveled edges for orbital welding. – Sanitary Fittings: Ends may be expanded or swaged for tri-clamp, butt weld, or sanitary flanges. 7. Cleaning & Inspection – Ultrasonic Cleaning: Removes residual contaminants. – Non-Destructive Testing (NDT): – Eddy Current/Ultrasonic Testing for defects. – Hydrostatic/Pneumatic Testing for leaks. – Dimensional Checks: OD, ID, wall thickness, and straightness per ASTM A270. 8. Certification & Packaging – Mill Test Reports (MTRs) verify compliance with ASTM A270 (chemical composition, mechanical properties). – Sterile Packaging: Tubes are sealed in plastic or protective caps to prevent contamination.
Sanitary Fittings in Process Piping (Food, Pharma, Dairy, etc.)
In industrial contexts, Sanitary Fittings (or Hygienic Fittings) refer to the specialized components used to connect pipes in systems where purity and cleanliness are critical. They are designed to prevent bacterial growth, allow for complete cleaning, and ensure product integrity.
Key Idea: These are the connectors and pipes themselves, used to build a system for processing sensitive products.
Key Characteristics:
Smooth, Polished Surfaces: Internally, they have a very smooth finish (often measured in Ra micro-inches) to prevent bacteria from clinging and to allow for easy cleaning.
No Crevices or Dead Spaces: They are designed to be flush with the pipe, creating a seamless flow path so that product or cleaning fluids don’t get trapped.
Easy to Disassemble and Clean (CIP/SIP): They are designed for frequent cleaning, often using methods like Clean-in-Place (CIP) or Sterilize-in-Place (SIP).
Material: Almost exclusively made from 304 or 316L Stainless Steel for its corrosion resistance and non-reactivity.
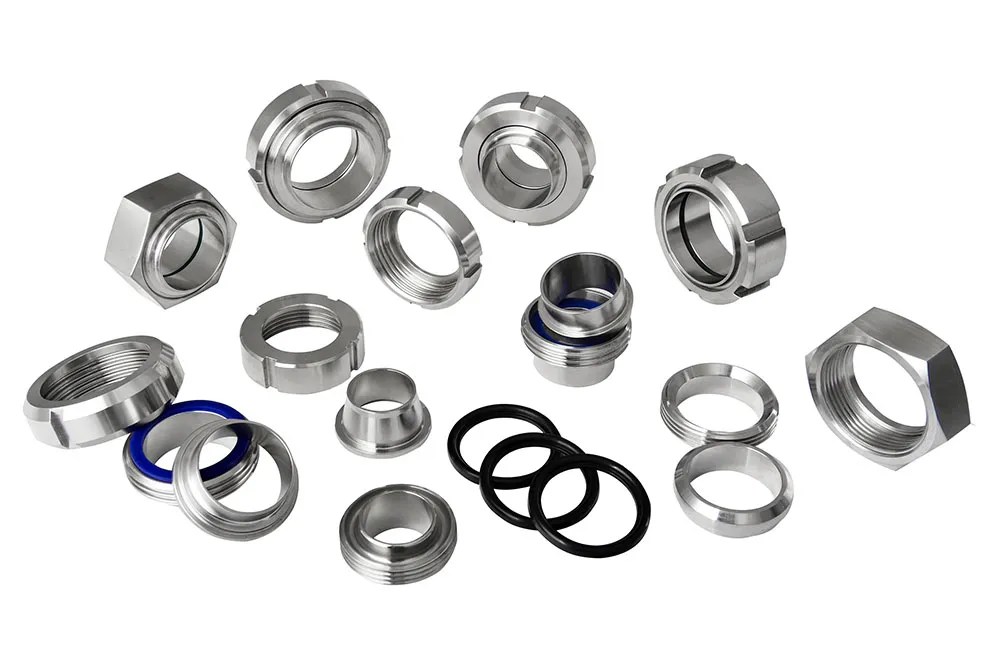
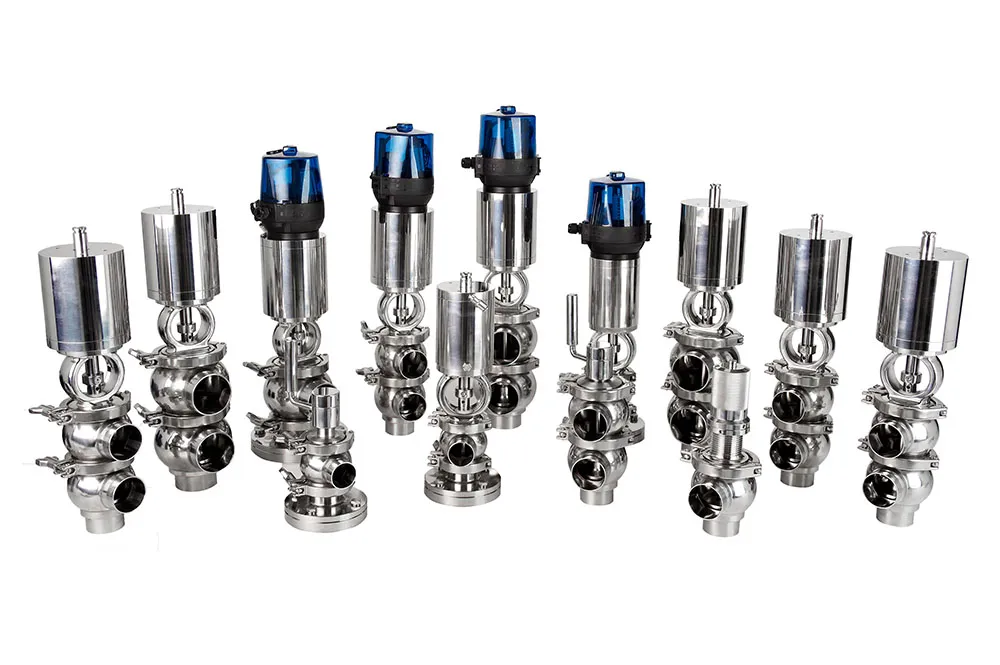
Common Types of Sanitary Fittings:
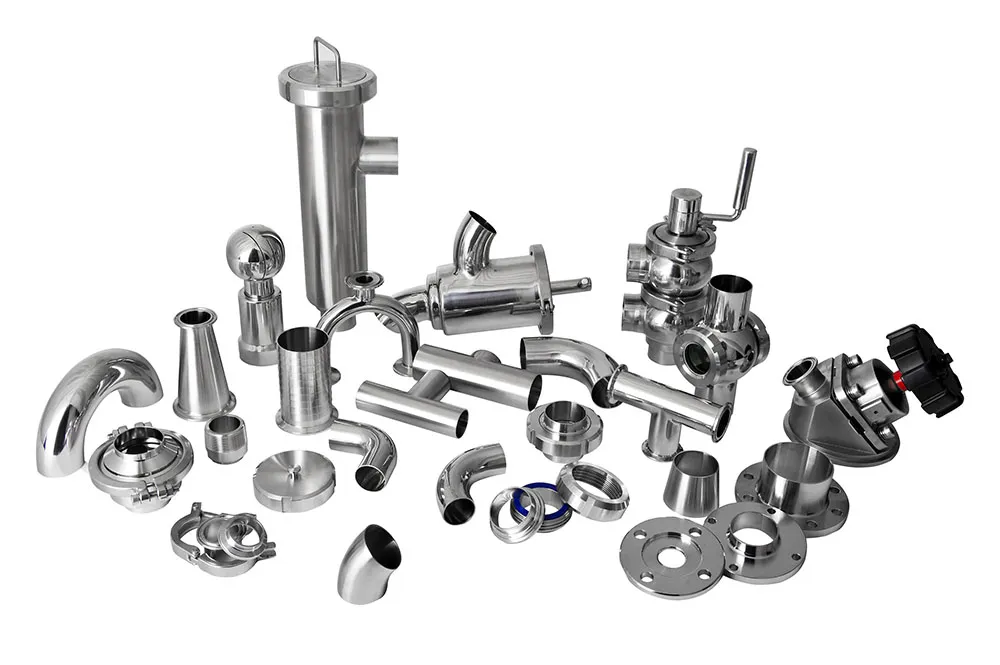
Clamp Fittings (Tri-Clamp): The most common type, using a three-piece clamp to seal a gasket between two ferrules.
Butt Weld Fittings: Permanently welded to create a perfectly smooth, crevice-free joint. Used where disassembly isn’t needed.
Bevel Seat Fittings: An older style, similar to clamp fittings but with a different gasket and connection system.
DIN/SMS Fittings: Standards more common in Europe, using a threaded nut to compress a gasket.
Common Components:
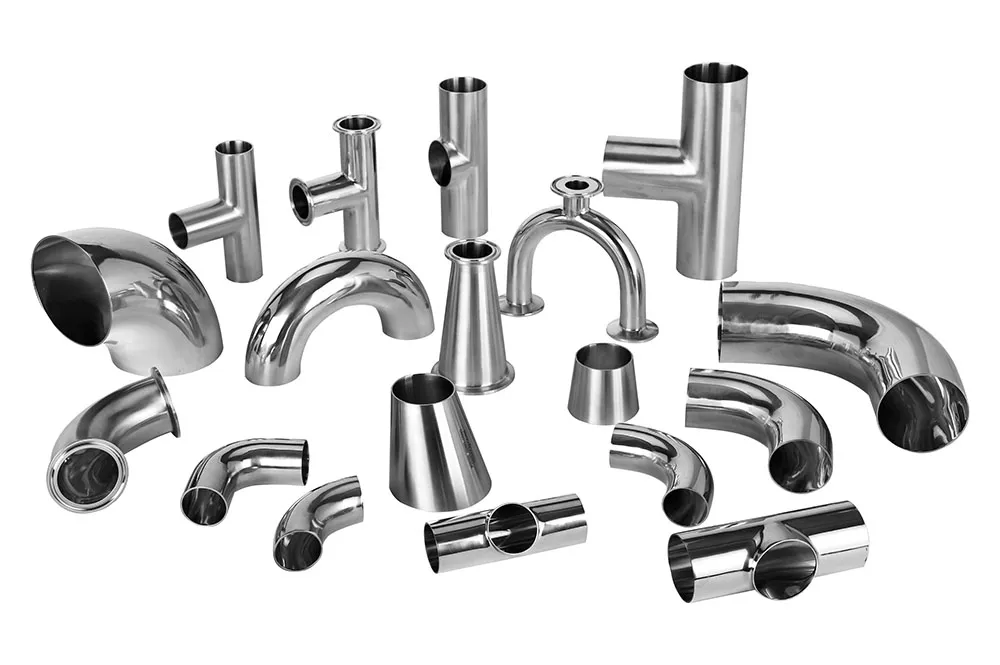
Elbows (90°, 45°)
Tees
Reducers
Caps
Ferrule (the stub end that gets connected)